

Build layout defines the orientation, position, spacing, quantity and identification of models in a wax-printing job. It affects printing time as well as cleaning, inspection and sorting. Judge efficiency by the number of acceptable models delivered in the available time, rather than whether the build area is full.
A useful layout must meet printing conditions while protecting models and fitting downstream capacity. When several designs share a build, every printed model must remain linked to its version and order, so sorting does not consume the time saved during printing.
Define the Objective of the Print Job
Repeated tasks of stable styles, verification tasks of multiple new products, and replacement tasks with tight deadlines may have different priorities. The quantity, delivery time, quality requirements and trial production purpose should be clarified before typesetting.
If this round is used to verify the impact of direction on a certain detail, comparable arrangements should be retained; if it is used to deliver multiple orders, completion time and post-processing sequence should be considered. You cannot simply compare which layout is more fulfilling without a goal.
Print batches also do not have to be identical to customer orders or casting batches. Models that can be printed together may differ in delivery status, target alloy, or subsequent processing schedule. Typesetting should support subsequent sorting, rather than allowing models to be used for different purposes to lose their identity.
Orientation and Height Affect Job Planning
The pose of the model will change the build height, arrangement of auxiliary materials, and treatment relationships of certain surfaces. The specific effects of different equipment and material systems vary and should be evaluated using actual software and process information.
3D Systems’ MJP technical note explains how construction is done by depositing material through a nozzle. Its public page includes wax and other material systems. Specific tasks should still be matched according to the corresponding equipment and materials. The processing rules for one material cannot be applied to all MJP tasks. MJP technical description
When changing orientations on the same ring, check where important curves, settings and prongs will be. If the height is lowered, it will make subsequent pick-up and placement more difficult, or it will make it more difficult to observe key areas, and the final efficiency may not be improved.
Fixed tilt angles are not a substitute for actual model evaluation. Software estimates can help compare options but should be coupled with testing of real results. The applicable conditions of existing solutions should also be recorded, such as style version, quantity, mode and delivery status.
Spacing Must Support Printing and Post-Processing
The distance between adjacent models must first meet the actual equipment and software requirements. At the same time, whether the model is easy to identify, pick up, and clean should also be considered. You cannot assume that all spacing will be appropriate based on a full-page image.
There should be an operating space around vulnerable models that is suitable for the handling method. For long poles, twigs and overhanging structures, the relationship between them and adjacent models should be checked to avoid mutual involvement during separation or transportation.
Material properties also need to be taken into consideration. 3D Systems’ Red Jewelry Wax material page emphasizes application characteristics related to detail performance and processing strength, but it cannot provide safe spacing for all devices or all geometries. Red jewelry wax material introduction
If the software supports a particular arrangement, the actual limitations should be confirmed with the device documentation. Just because the interface can be stacked up and down does not mean that the current system and post-processing process are suitable for this task.
Check Job Compatibility Before Filling the Build
Models sharing a task should use compatible materials and construction conditions, and be able to accept corresponding completion times. Tasks that require different modes or different delivery statuses should first be evaluated as to whether they can be combined.
When complex new products and stable styles are mixed, attention should be paid to whether trial production changes will affect the entire batch delivery. If a new structure needs to be explored, its verification purpose should be reflected in the design, and unconfirmed geometry should not be treated directly as a mature style.
The quantity and identity of the replacement parts should also be stated. If dozens of spare parts are not marked, they may be mistaken for official delivery; if the old version is left in the build file, it may be output again the next time it is reused. Before submitting each task, the model list should be checked against the actual layout.
To determine whether to merge tasks, it is advisable to compare the estimated completion time, post-processing capabilities, and recognition complexity at the same time. If a larger batch of output takes a long time to wait for cleaning, the time saved on the machine side may not translate into actual delivery benefits.
Include Post-Processing Capacity in Efficiency
After printing, the model needs to be cleaned, inspected and packaged as agreed. A sudden increase in single output may make post-processing a waiting step. Typesetting arrangements should be coordinated with post-processing personnel, tools and delivery sequence.

Fragile styles require more careful handling and inspection. If multiple small models are tightly packed together, separation and identification may increase the operational burden. Clearer partition or position numbers can help teams process things in order.
This does not mean that fixed partitioning is necessarily best. For some tasks, other arrangements may be more appropriate; actual operations and results need to be recorded before judging whether to retain the plan. Typographic optimization should focus on real bottlenecks rather than following a neat-looking format.
Post-processing feedback is best directed at specific locations and actions. For example, which row of models is difficult to grab, what kind of details are easily encountered by adjacent structures, and what kind of logos are lost after cleaning. Such information can be directly used for next adjustment.
Prevent Mix-Ups with Traceable Identification
Whether the model is allowed to be numbered should be confirmed by the design and craftsmanship personnel. The location of the marking must not affect appearance, fit or critical dimensions, nor may it create unidentified additional structure that needs to be removed.
When marking on the model is not suitable, location maps, container numbers and sorting records can be used. The key is to maintain the corresponding relationship before and after cleaning. After the model leaves the original layout, the position map may lose its function if there is no supporting operation record.
It is especially easy to confuse the task of wearing the same ring with different circumferences and the same shape with different words. The identification method should be written in the task order and checked again during packaging. Don’t leave the entire responsibility of discernment to the recipient.

Comparing Two Build Layouts
| Compare items | What should be recorded |
|---|---|
| Enter conditions | Same versions, quantities, materials and comparable models |
| Main changes | Factors in epicycle adjustment in direction, position, or spacing |
| software estimation | Estimated time and related task information |
| actual build | Actual start and end time and exceptions |
| Post-processing | Manual operation time, waiting and processing difficulties |
| Qualified output | Original qualified, qualified and scrapped quantity after allowed repair |
| Deliver results | Whether the model is completed on time and in the specified state |
If you want to judge the impact of a certain factor, you can make other conditions as comparable as possible. The two tasks change the direction, quantity and mode at the same time. Even if the results are different, it cannot be directly concluded that a certain direction is faster or more stable.
Software estimates and actual times should be saved separately. It is also necessary to avoid repeated counting of the qualified quantity: the reworked model is part of the output of the batch and should not be repeatedly added to the original qualified number. Real records are more useful than unverified efficiency percentages.
It is possible to record “number of qualified deliverables ÷ total task duration” and “manual operation time ÷ number of qualified deliverables” at the same time. The former observes the delivery rhythm, while the latter observes labor input; reprinting, rework and waiting are recorded separately. The estimated construction time of the software cannot be regarded as the entire duration, nor can the parallel work hours of multiple people be directly added to the duration.
Check Changes Before Reusing a Layout
Old tasks can be used as a starting point, but first check version, quantity, mode and delivery requirements. Local structural modifications may change the height, support and handling difficulty; quantitative changes may affect the layout and post-processing rhythm.
It is recommended to indicate the purpose of the stabilization plan and the exploration plan respectively. When using the old scheme, record whether this round is still within the original verification scope; changes outside the scope should be re-evaluated. In this way, typesetting experience can be reused under clear conditions.
Improve the Layout from Sorting Feedback
If there are multiple perimeters for the same task and it is inconvenient to distinguish them after cleaning, you can check whether the original location map is still valid after separation. The next round can evaluate the partition, container number or approval mark and schedule corresponding actions.
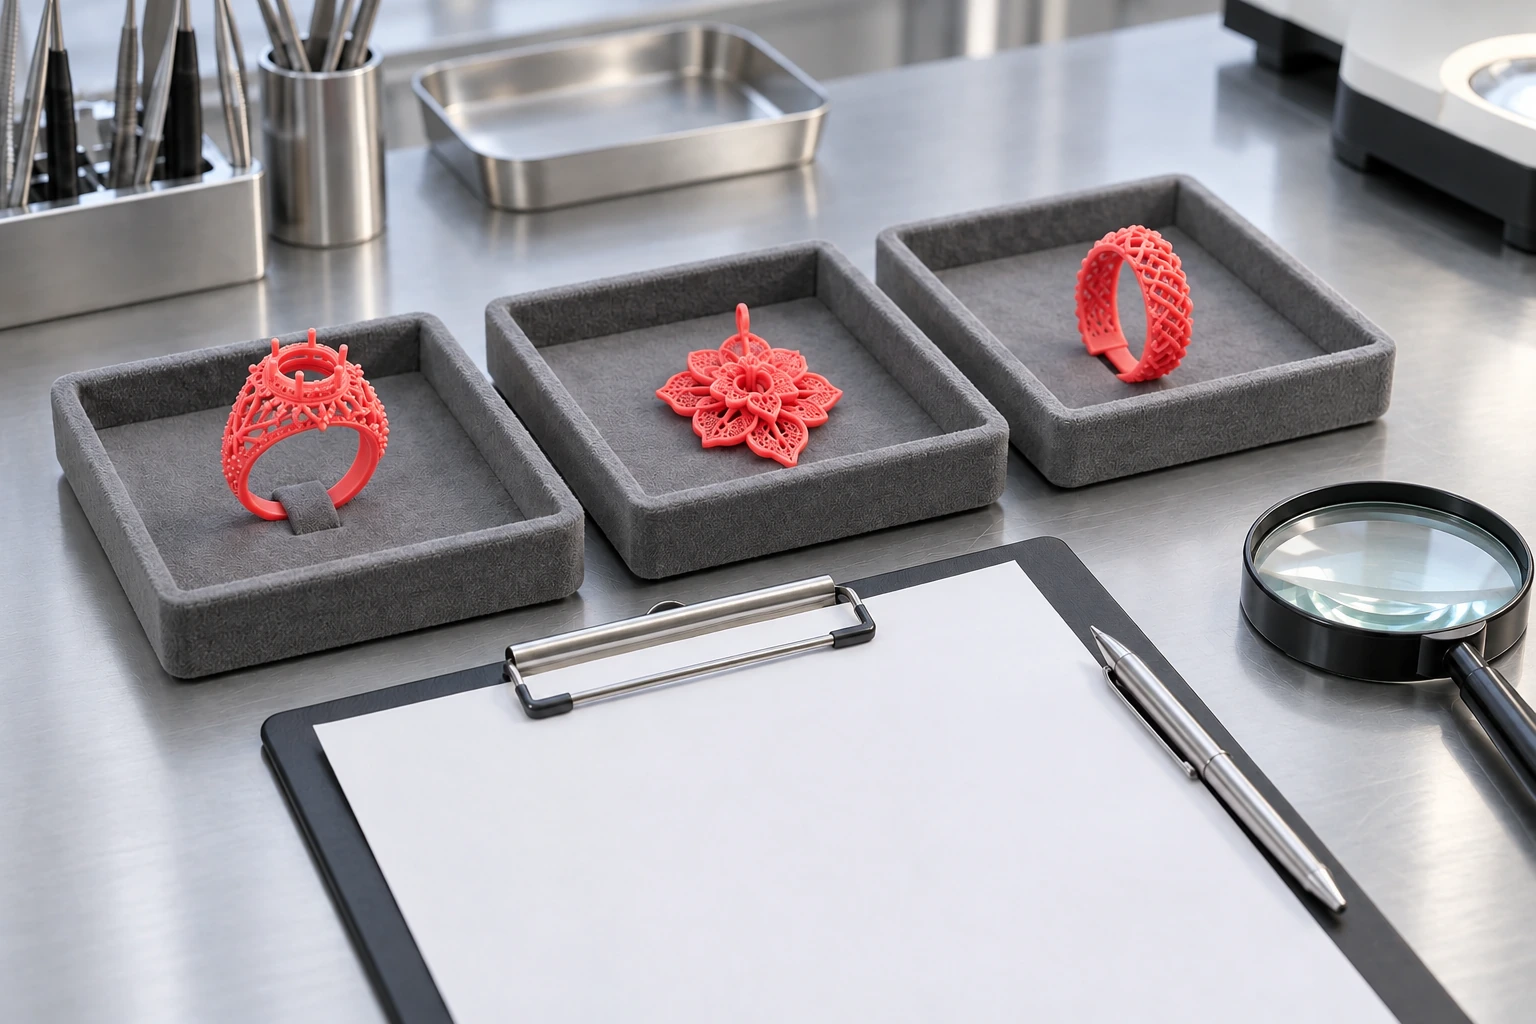
The new way to confirm identity is to keep it all the way to the package, rather than just making the build screenshots neater. If the number and spacing of partitions are changed, task estimates and processing space should also be rechecked, and recognition improvements should be evaluated together with actual efficiency.
Frequently Asked Questions
Does Placing Every Model Lower Always Print Faster?
Build height may affect time, but the complete task is also affected by factors such as equipment mode, geometry and ancillary structures. Actual software estimates should be compared and checked against post-processing results with real output.
How Does Build Layout Differ from Multi-Order Scheduling?
Typesetting focuses on the arrangement of models within a single build; scheduling focuses on the order, delivery dates, and resources of multiple batches of tasks. The two need to cooperate, but one full version cannot be used to represent the production efficiency of the entire month.